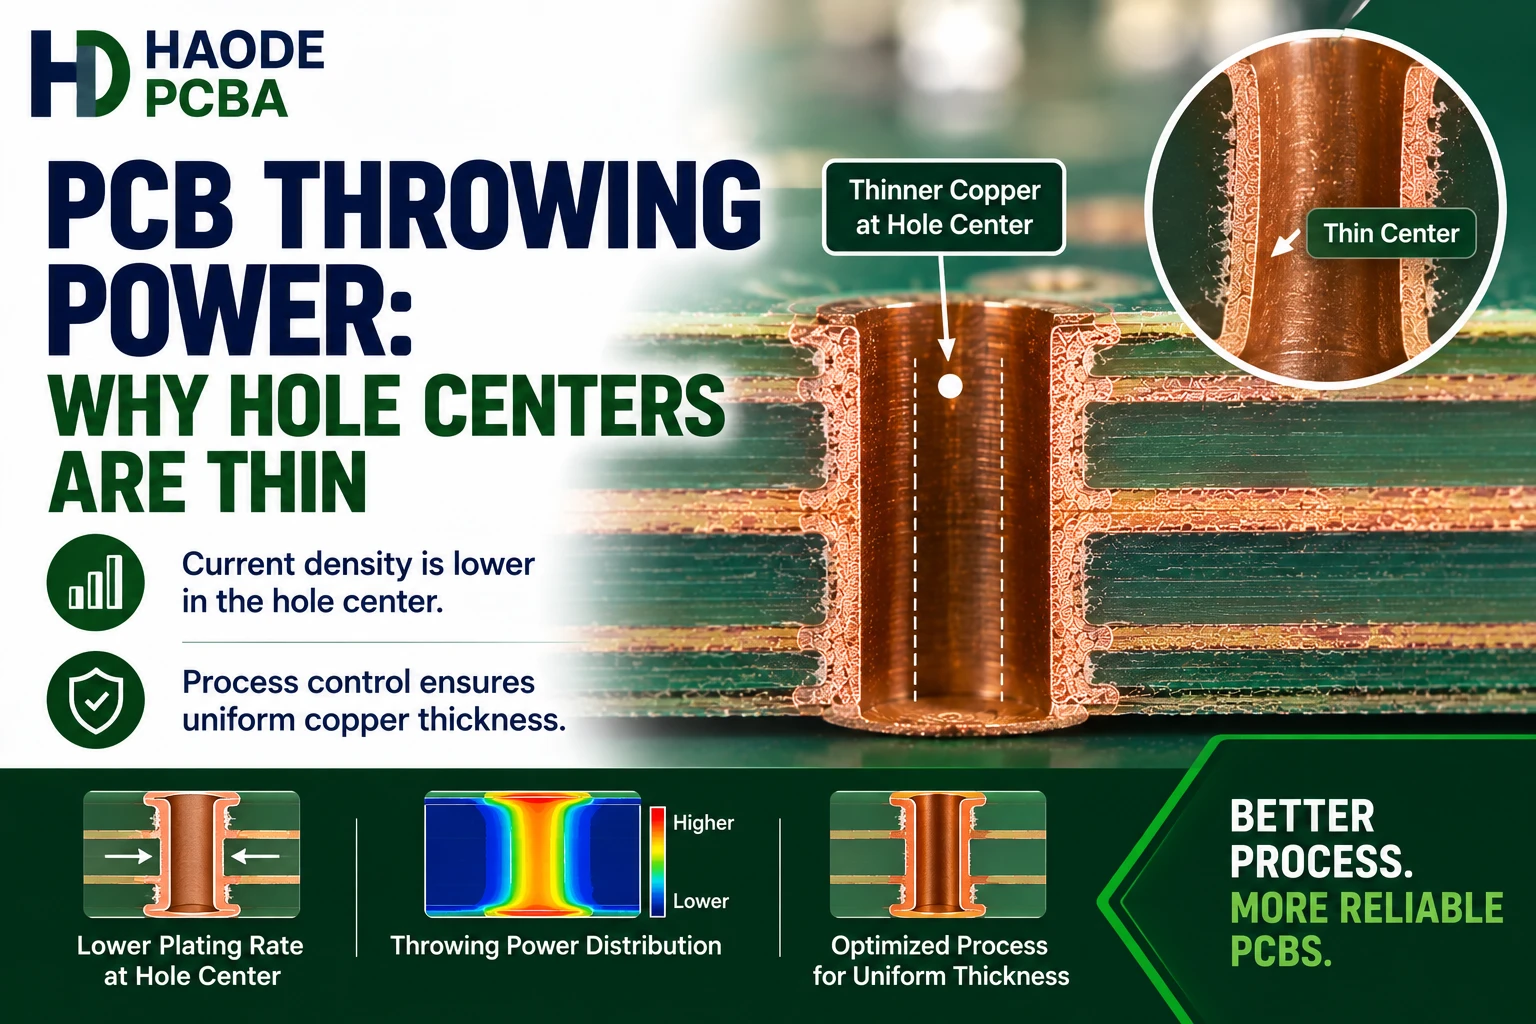
PCB throwing power describes how effectively an electroplating process deposits copper inside a through hole compared with the board surface. Poor throwing power creates thick copper near the hole entrances and thinner copper at the hole center, where inspection and solution exchange become more difficult.
However, throwing power is a distribution ratio—not a finished-board acceptance result. Buyers must evaluate both the percentage and the actual minimum copper thickness at the critical hole location.
What Is PCB Throwing Power?
PCB throwing power measures the ability of a plating process to distribute copper into recessed areas such as through holes.
During electroplating, electrical current reaches exposed outer surfaces more easily than the center of a deep hole. Therefore, copper normally deposits faster on the board surface and near the hole entrances.
A high-throw plating process reduces that difference.
Uyemura describes the central challenge as meeting the required minimum copper thickness at the center of a high-aspect-ratio hole. Likewise, the Global Electronics Association includes mechanical factors, chemistry, shielding, eductors, and pulse plating among the variables that affect plating distribution and throwing power.
Before electrolytic plating begins, PCB electroless copper must create a continuous conductive layer on the hole wall. Throwing power then describes how the subsequent electroplating process builds copper over that conductive layer.
How Is PCB Throwing Power Calculated?
A simplified calculation is:
PCB Throwing Power (%) = Average Hole-Center Copper Thickness ÷ Average Surface Copper Thickness × 100
For example:
- Average surface copper deposit: 25 µm
- Average hole-center copper deposit: 18 µm
The calculated throwing power is:
18 ÷ 25 × 100 = 72%
This means the hole center received approximately 72% of the copper deposited at the selected surface measurement points.
However, laboratories do not always use identical measurement locations. One method may compare the hole center with the board surface. Another may use multiple surface, entrance, and center measurements.
Therefore, a report should define:
- Measurement-point locations
- Number of measurements
- Whether values represent averages or minimums
- Whether base copper has been subtracted
- Microsection preparation method
- Magnification and measurement system
- Calculation formula
- Acceptance criterion
Without this information, two suppliers can report different throwing-power values from similar copper profiles.
Why Does 100% Throwing Power Not Guarantee a Good PCB?
Throwing power expresses relative distribution. It does not prove that the actual copper thickness meets the drawing requirement.
Consider two plated holes:
| Example | Surface Deposit | Hole-Center Deposit | Throwing Power | Possible Interpretation |
|---|---|---|---|---|
| Hole A | 12 µm | 12 µm | 100% | Excellent distribution, but copper may be too thin |
| Hole B | 36 µm | 25 µm | 69% | Lower distribution ratio, but center thickness may meet the requirement |
| Hole C | 30 µm | 15 µm | 50% | Thin center and excessive surface buildup |
| Hole D | 24 µm | 21 µm | 88% | Balanced profile with useful absolute thickness |
If a drawing requires more than 12 µm of finished hole copper, Hole A fails despite its 100% throwing power.
Therefore, buyers should request both:
- The throwing-power calculation
- The minimum finished hole-wall copper thickness
This distinction prevents a process-control percentage from replacing the actual product requirement.
Why Is Copper Thinner at the Hole Center?
The hole center experiences a more difficult electrochemical environment than the board surface.
Electrical Resistance
Current must travel through a narrow plated structure. As the hole becomes deeper and smaller, electrical resistance and current distribution become less favorable at the center.
Restricted Solution Exchange
Fresh copper ions and plating additives must reach the center of the hole. Meanwhile, reaction products must leave.
Restricted exchange can create different conditions at the hole entrance and center.
Additive Behavior
Acid copper chemistry normally contains proprietary additives that control deposition, grain structure, leveling, and surface appearance.
Their behavior depends on:
- Concentration
- Current density
- Solution movement
- Temperature
- Chloride level
- Organic breakdown products
- Bath age
- Carbon treatment or purification history
The outer surface and hole center do not experience identical flow and electrical conditions. Consequently, additives can affect those regions differently.
Current Crowding
Edges, corners, isolated pads, and hole entrances can attract more current. These locations may plate faster while recessed areas receive less copper.
Panel Pattern Density
Large copper areas, sparse regions, and different hole populations can distribute current unevenly across a panel.
Thus, local design density can affect the result even when the plating bath remains within its chemical limits.
How Does Aspect Ratio Affect PCB Throwing Power?
Aspect ratio compares board thickness with drilled-hole diameter.
A thicker board or smaller hole increases the distance that chemistry and current must reach. Therefore, throwing power generally becomes more difficult as the PCB aspect ratio increases.
Risk also rises when a design combines:
- Thick finished boards
- Small mechanical drills
- Dense through-hole arrays
- Heavy finished copper
- High layer counts
- Mixed hole diameters
- Large panel dimensions
- Uneven copper distribution
However, one aspect-ratio number does not describe the complete plating challenge.
For example, two 10:1 holes may respond differently if they use different:
- Laminate materials
- Hole diameters
- Panel locations
- Drilling conditions
- Copper patterns
- Plating equipment
- Current programs
Therefore, the supplier should qualify the actual board geometry rather than relying only on a published maximum aspect ratio.
What Is a Dog-Bone Copper Profile?
A dog-bone profile occurs when copper becomes thick at both hole entrances but remains thinner through the center.
In cross-section, the two thick ends resemble the ends of a bone.
A dog-bone profile can indicate:
- Poor throwing power
- Excessive current density
- Weak solution exchange
- Unsuitable plating chemistry
- Additive imbalance
- Inadequate panel movement
- Poor anode or shield configuration
- Challenging hole aspect ratio
Adding more plating time may increase center copper. However, it also adds copper to the already thick surfaces and entrances.
Consequently, the factory may create:
- Excessive surface copper
- Narrower trace spacing
- Greater etching difficulty
- Increased copper consumption
- Longer production time
- Reduced fine-line capability
The relationship between plated surface copper and later conductor geometry should also be reviewed through the PCB etch factor.
Which Process Variables Control PCB Throwing Power?
Throwing power results from the complete plating system rather than one bath setting.
| Process Variable | Possible Effect on Hole-Center Copper |
|---|---|
| Current Density | Excessive current may favor surfaces and hole entrances |
| Plating Time | Adds copper but may not correct the distribution ratio |
| Copper Concentration | Changes deposition behavior and process capability |
| Acid And Chloride Control | Influences conductivity and additive performance |
| Organic Additives | Control suppression, acceleration, leveling, and deposit structure |
| Solution Movement | Improves exchange through the hole |
| Panel Movement | Changes local flow and boundary-layer conditions |
| Anode Position | Affects current distribution across the panel |
| Shields And Robbers | Redirect current away from high-current regions |
| Electrical Contacts | Poor contact creates panel-to-panel or rack-position variation |
| Bath Temperature | Influences deposition and additive behavior |
| Filtration | Helps control particles and bath contamination |
| DC Or Pulse Program | Changes deposition behavior and equipment requirements |
MacDermid Alpha’s high-throw acid copper information emphasizes the relationship among current density, high-aspect-ratio features, copper distribution, and process productivity.
A factory should not change one variable without checking deposit ductility, tensile behavior, surface thickness, fine-feature capability, and production time.
Can Copper Thieving Improve Throwing Power?
Copper thieving can help balance current distribution across a panel by adding nonfunctional copper to selected low-density areas.
This may reduce excessive plating in sparse regions and improve panel-level uniformity. However, thieving does not directly guarantee better copper at the center of every hole.
The result depends on:
- Thieving location
- Copper pattern density
- Connection to the plating circuit
- Panel rails
- Anode arrangement
- Shielding
- Hole distribution
- Plating method
Therefore, PCB copper thieving should support the complete panel-plating strategy. It should not serve as a generic decoration added to every empty area.
Functional copper must also remain under customer control. The fabricator should not alter signal, RF, isolation, impedance, or high-voltage regions without approval.
How Do DC and Pulse Plating Compare?
Direct-current plating applies current in one continuous direction. Pulse plating changes current over time, while pulse-reverse systems may include controlled reverse-current periods.
| Method | Potential Advantage | Main Tradeoff |
|---|---|---|
| Conventional DC | Familiar equipment and straightforward control | May require lower current or longer time for difficult holes |
| High-Throw DC | Better deep-hole distribution without pulse equipment | Depends heavily on chemistry and process control |
| Pulse Plating | Can improve deposit distribution and grain control | Requires suitable rectifiers and qualified parameters |
| Pulse-Reverse Plating | May improve difficult via or hole profiles | Adds process and equipment complexity |
Pulse plating is not automatically necessary for every high-aspect-ratio board. Modern DC chemistry may provide suitable results for many constructions.
Conversely, owning pulse equipment does not prove that the factory can plate the customer’s board. Qualification data must cover the actual aspect ratio, material, pattern density, and copper requirement.
How Should PCB Throwing Power Be Measured?
The manufacturer normally prepares a plated coupon or production-board sample as a microsection.
A reliable measurement requires the laboratory to:
- Cut through the approximate center of the hole.
- Mount the specimen without damaging the barrel.
- Grind and polish the sample.
- Confirm that the section passes through the true hole center.
- Measure copper at defined surface, entrance, quarter, and center locations.
- Record individual and average values.
- Apply the agreed calculation.
- Retain calibrated images with measurement markers.
Evident Scientific’s explanation of throwing-power image analysis describes an 11-point microsection measurement method. However, one commercial measurement scheme should not automatically become every project’s acceptance rule.
The buyer and supplier must agree on the method used for the actual report.
What Can Make a Throwing-Power Measurement Misleading?
Several errors can distort the result.
The Section Misses the Hole Center
If the laboratory sections away from the true diameter, the apparent wall geometry and copper thickness can change.
Base Copper Is Included Incorrectly
Surface measurements may include both starting foil and deposited copper. Meanwhile, hole-wall measurements represent plated copper.
Unless the calculation defines how to treat base copper, the comparison may become invalid.
Averages Hide the Minimum
An average center thickness can pass while one local measurement remains below the specified minimum.
Therefore, reports should provide raw measurements rather than only one percentage.
The Coupon Does Not Represent the Product
A low-aspect-ratio coupon placed near the panel edge may not represent the smallest hole or most difficult panel location.
Sample Preparation Smears Copper
Poor polishing can drag copper across an interface or round the specimen edge. As a result, the measured layer can appear thicker or more continuous than it is.
A controlled PCB microsection must document sample location, preparation method, magnification, and calibrated measurements.
Is 80% PCB Throwing Power Acceptable?
An 80% target appears in some industry measurement practices. However, it is not a universal acceptance limit for every PCB.
The acceptable value depends on:
- Minimum hole-wall copper requirement
- Starting surface copper
- Final surface copper limit
- Hole aspect ratio
- Product reliability class
- Fine-line requirements
- Plating method
- Customer drawing
- Applicable specification and revision
For example, 80% throwing power can still fail if the absolute center thickness remains below the requirement.
Likewise, a lower percentage may still produce sufficient center copper, although it may increase surface copper, etching difficulty, cost, and process variation.
Therefore, the product drawing should control minimum copper thickness. The throwing-power percentage should support process qualification and ongoing control.
How Does Poor Throwing Power Affect Reliability?
Thin hole-center copper creates the weakest barrel region.
During soldering and operation, the laminate expands more in the Z-axis than copper. This places cyclic strain on the plated barrel.
If the center copper lacks sufficient thickness or suitable mechanical properties, the PCB may develop:
- Resistance increase
- Intermittent circuits
- Circumferential barrel cracks
- Corner cracks
- Open circuits after thermal cycling
- Early failure during rework
- Reduced field life
However, copper thickness alone does not explain every PCB barrel crack. Investigators must also examine copper ductility, grain structure, drilling quality, laminate expansion, hole geometry, and thermal history.
Poor throwing power also differs from PCB plating voids. A thin but continuous deposit is a distribution problem, while a void represents missing or discontinuous copper.
Similarly, PCB interconnect defects occur at specific copper interfaces and may involve contamination or adhesion rather than insufficient barrel thickness.
PCB Throwing Power Troubleshooting Matrix
| Observed Pattern | Likely Area To Investigate | Evidence To Request |
|---|---|---|
| Thin Center in Most Holes | Chemistry, current density, flow, or aspect ratio | Bath analysis, current program, representative sections |
| One Panel Edge Plates Thin | Anode position, shielding, contact, or flow | Panel map and rack-position data |
| Small Holes Fail but Large Holes Pass | Geometry and solution exchange | Hole-size comparison |
| Surface Copper Becomes Excessive | Low throwing power compensated by extra plating time | Surface and center thickness records |
| Hole Entrances Are Very Thick | Current crowding or poor distribution | Entrance, center, and surface measurements |
| Thickness Varies by Lot | Bath age, additives, loading, or maintenance | Statistical process data |
| Copper Is Continuous but Cracks After Stress | Thickness, ductility, or thermal mismatch | Post-stress sections and material data |
| Isolated Areas Have No Copper | Pretreatment or primary metallization | Desmear, activation, and electroless copper evidence |
This matrix narrows the investigation. Nevertheless, the supplier should confirm the suspected mechanism with measurements from affected and unaffected samples.
What Should Buyers Specify?
A useful fabrication requirement should define the product result rather than only a throwing-power percentage.
Buyers should specify:
- Minimum finished hole-wall copper
- Applicable PCB class
- Governing specification and revision
- Critical hole sizes
- Finished board thickness
- Required microsection locations
- Sampling plan
- Thermal preconditioning
- Reporting requirements
- Whether raw measurement values are required
- Any agreed throwing-power calculation
A practical note could state:
Measure finished hole-wall copper at the defined entrance, quarter, center, and corresponding opposite-side locations. Report individual values, minimum thickness, surface deposit thickness, calculation method, and throwing-power percentage. Product acceptance remains subject to the specified minimum hole-wall copper requirement.
The project team should adjust this wording to match the relevant contract and standard.
PCB Throwing Power DFM Checklist
Before releasing the design, confirm:
- What is the smallest drilled hole?
- What is the finished board thickness?
- What is the maximum aspect ratio?
- Which holes create the greatest plating challenge?
- Does the supplier have qualified data for this geometry?
- What minimum hole-wall copper does the drawing require?
- Will excessive surface buildup affect fine-line etching?
- Does the panel contain strongly unbalanced copper density?
- Are plating thieves, shields, or robbers necessary?
- Does the coupon represent the most difficult hole?
- Are measurement locations defined?
- Does the report include raw thickness values?
- Is the throwing-power formula stated?
- Does the thermal test represent assembly exposure?
- Are material and stackup substitutions controlled?
These checks belong in the broader PCB DFM checklist because hole geometry, panel layout, copper requirements, and fabrication capability must work together.
Final PCB Throwing Power Recommendation
PCB throwing power explains how evenly copper reaches the center of a plated through hole. It does not replace the minimum hole-wall copper requirement.
For reliable supplier evaluation:
- Check both percentage and absolute thickness.
- Define the calculation and measurement points.
- Use coupons that represent the most difficult production holes.
- Compare surface, entrance, and center copper.
- Review panel position and pattern density.
- Confirm chemistry and equipment capability for the actual aspect ratio.
- Investigate voids, thin copper, and interface separation as different defects.
- Verify critical constructions after representative thermal stress.
The essential relationship is:
Hole Geometry + Panel Current Distribution + Chemistry + Solution Movement → PCB Throwing Power → Minimum Hole-Center Copper → Thermal Reliability
This evidence allows buyers to distinguish a genuinely capable plating process from a report that presents one favorable percentage without showing the copper thickness that matters most.